
Blog
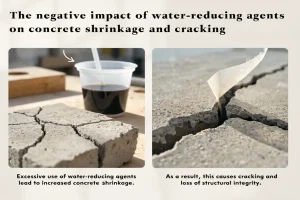
The negative impact of water reducing agents on concrete shrinkage and cracking
Blog The negative impact
Blog
In modern concrete technology, chemical concrete admixtures—including high-range water reducers (superplasticizers), retarders, accelerators, and air-entraining agents—are indispensable. Although typically dosed at merely 0.5% to 2.5% of total cementitious material mass, their chemical influence over concrete workability, rheology, setting kinetics, and ultimate compressive strength is decisive.
However, the high chemical potency of admixtures makes them unforgiving of operational carelessness. Minor errors in storage, dispensing, or jobsite remediation can trigger catastrophic structural defects:
This comprehensive technical guide details the three critical operating pillars every batching plant and site engineering team must enforce to ensure consistent, high-performance concrete production.
Most liquid chemical concrete admixtures are water-based solutions, emulsions, or suspensions containing organic polymers (such as polycarboxylate ethers, lignosulfonates, or naphthalene sulfonates) and inorganic salts.
During prolonged storage in bulk tanks:
If liquid is drawn directly from an unagitated tank:
To maintain chemical homogeneity across every batch:
Although the dosage of additives is small, they have a huge impact on the performance of concrete. If there is a problem with the weighing hopper and the dosage is too large, it is not only uneconomical, but may also cause serious engineering quality accidents.
If the amount of wood calcium is greater than 0.5% of the cement mass, it will introduce excessive air and slow down the initial setting, reducing the early strength of the concrete. The same is true for sugar syrup and humic acid water reducers, and even the concrete does not set and harden for several days. There have been many accidents caused by this in China. For example, a certain mixing plant supplied concrete to a construction site, but one floor did not harden. After it was destroyed, the mixing plant compensated more than 400000 yuan.
During transit from the batching plant to the construction site, concrete frequently suffers significant slump loss due to extended transport distances, traffic congestion, elevated ambient temperatures, or extended pump waiting times.
Under no circumstances should truck drivers or site laborers add unmetered water to the mixing drum (“water trimming”). Adding just 10–15 liters of unauthorized water per cubic meter can:
When concrete arrives on site with inadequate workability for pumping or placement, the secondary fluidization method (post-dosing water reducer) must be executed:
Liquid admixtures are complex aqueous formulations containing dispersed polymers, organic salts, and stabilizing agents. Over time, gravity causes insoluble components and denser molecular chains to settle toward the bottom, forming a density gradient that causes underdosing at the top and overdosing at the bottom.
Calcium lignosulfonate acts as both a set retarder and a surfactant. When dosed beyond 0.5% by cement mass, it entrains excessive, non-uniform air bubbles into the paste and severely retards early hydration, causing significant drops in early and 28-day compressive strength.
Secondary fluidization introduces a controlled dose of high-range water reducer (superplasticizer) into the transit mixer drum at the jobsite. The chemical restores electrostatic and steric dispersion between cement grains without adding water, allowing the mix to regain pumpable slump while preserving the design water-cement ratio and strength.
The truck mixer drum must rotate at maximum high speed (12–16 rpm) for at least 2 full minutes after the chemical admixture is introduced to ensure complete, uniform dispersion throughout the entire batch volume before discharging.
The negative impact of water reducing agents on concrete shrinkage and cracking
Blog The negative impact
Impact of Polycarboxylate Superplasticizer Macromonomer Molecular Weight on PCE Powder
Blog Impact of Polycarbox
Discussion of the room temperature process and precautions for PCE in case studies
Blog Discussion of the ro
Product information, specifications & applications — sent directly to your email.
*Your information is kept confidential and will only be used to contact you regarding our products.